How Does an EDI Water System Work in 2026?
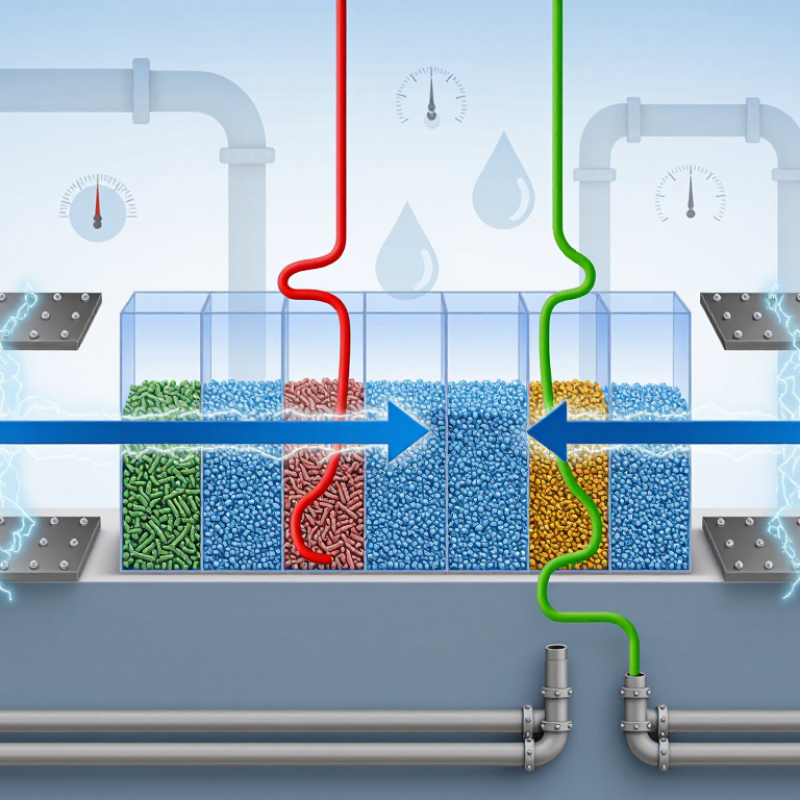
In 2026, an Edi Water System can turn reverse-osmosis permeate into high-purity water without routine chemical regeneration. Understanding the EDI Water System Working Principle starts with the module itself: alternating ion-exchange membranes and resin-filled compartments sit between electrodes. A controlled electric current draws dissolved ions through the membranes and into concentrate channels. The purified stream continues toward the product outlet. A small detail matters: feed water quality affects how steadily the system performs.
Water-treatment consultant Peter S. Cartwright has written about electrodeionization, but no source text was provided here to verify a verbatim quotation. A careful, non-verbatim summary of the principle is: “EDI uses electricity, ion-exchange media, and selective membranes to remove ions continuously.” In practice, operators still watch conductivity, flow, pressure, and feed-water conditions. Poor pretreatment can shorten run stability or compromise product quality. EDI is not magic. It is a precise process with limits, and real plants rarely behave as neatly as diagrams suggest. A closer look at each stage helps explain what the technology can—and cannot—deliver.
What an EDI Water System Is and Where It Is Used
How Does an EDI Water System Work in 2026?
What an EDI Water System Is and Where It Is Used
An electrodeionization (EDI) water system removes dissolved ions from pretreated water. It combines ion-exchange resin, selective membranes, and a direct-current electrical field. In many installations, reverse osmosis comes first. The EDI stage then reduces remaining ionic contaminants without routine chemical regeneration. Water flows through narrow compartments, while charged ions move through membranes toward concentrate streams. The result can be high-purity water, but performance depends on feed quality and proper system design. Not magic.
EDI is used where consistent low-conductivity water matters. Examples include pharmaceutical production, power-generation boiler feed, laboratory work, and some electronics manufacturing. A plant may monitor conductivity or resistivity, pressure, flow, and voltage to spot changes. EDI does not remove every contaminant; dissolved gases, particles, and organic compounds may need separate treatment. Requirements also vary by process, so a suitable system should be selected with qualified water-treatment professionals.
Tips: Check the reverse-osmosis water feeding the EDI unit, and follow the equipment maker’s operating limits. Watch for gradual changes in product-water quality or pressure. A reading can look acceptable for a while, yet still deserve investigation. That detail is easy to miss.
How Feedwater Is Prepared Before Entering the EDI Module
How Does an EDI Water System Work in 2026?
Before water reaches an electrodeionization (EDI) module, it needs careful preparation. In many systems, pretreatment removes suspended particles and reduces hardness, while reverse osmosis lowers dissolved salts. The resulting permeate is then checked for conductivity, temperature, flow, and pressure. Small changes matter. Excess hardness can encourage scale, while unsuitable feedwater chemistry may reduce performance or damage the module. Exact limits depend on the equipment design, so operators should follow its technical specifications.
Tips: Check conductivity and flow routinely, not only during commissioning. Watch the pretreatment filters and softener for pressure changes or exhausted capacity. If readings drift, investigate upstream causes before adjusting the EDI unit. Keep a simple log; trends can reveal trouble earlier than a single measurement.
Some systems also need carbon treatment or degassing to control oxidants and carbon dioxide. The right steps depend on the source water and the selected process. A clear-looking stream is not necessarily suitable. That point is easy to overlook. Feedwater preparation can feel like routine plumbing, yet it sets the conditions for stable EDI operation. Even a well-maintained module cannot compensate for every upstream problem.
How Feedwater Is Prepared Before Entering an EDI Module
Filtration and softening help protect downstream equipment, while reverse osmosis removes most dissolved ions. In this illustrative example, conductivity falls from 500 µS/cm in raw feedwater to 15 µS/cm at the EDI inlet. Actual feedwater limits vary by EDI module and system design.
How Ion Exchange and Electricity Remove Dissolved Minerals
An EDI water system, or electrodeionization system, combines ion exchange resin, selective membranes, and direct current to remove dissolved minerals. It is commonly installed after reverse osmosis, where the lower salt load helps the EDI unit produce steadier water. Inside its stack, thin channels carry water past tiny resin beads. The beads give ions a workable route through the compartment.
As water flows, dissolved positively charged ions, such as calcium, move toward the cathode. Negatively charged ions, such as chloride, move toward the anode. Selective membranes let these ions pass into separate concentrate channels, away from the purified water stream. The resin temporarily captures ions and helps them migrate, even when the water has low conductivity. Near depleted regions, the electric field can split water into hydrogen and hydroxide ions. These ions help regenerate the resin continuously. No chemical regeneration cycle is normally needed.
The process still depends on feedwater quality and careful operation. A change in conductivity or silica levels can affect performance, so operators monitor water quality and system readings. Not magic, though. EDI does not remove every neutral compound or replace good pretreatment. That limitation is easy to overlook when focusing only on mineral removal.
How Product Water Quality Is Monitored and Controlled
How Does an EDI Water System Work in 2026?
How Product Water Quality Is Monitored and Controlled
An electrodeionization (EDI) system polishes pretreated water, usually after reverse osmosis. Electric current moves dissolved ions through selective membranes, while resin inside the module helps capture them. The resin is continually regenerated by the electric field, so routine chemical regeneration is generally unnecessary. The product water then flows to a storage tank or point of use. Small changes matter.
Quality control starts with continuous measurements. Online conductivity or resistivity sensors show whether ionic content is changing. Operators also track flow, pressure, temperature, and electrical readings, because a sudden shift can signal fouling, scaling, or a feed-water problem.
Depending on the application, silica and total organic carbon may need separate analyzers or laboratory tests; conductivity alone cannot reveal every contaminant. Set alarm limits around the actual process requirement, not a generic target.
Good instruments need calibration and sensible maintenance. A sensor coated with residue can quietly report a misleading value. Compare online readings with periodic grab samples, and check sample lines for stagnant water before trusting a result. A stable trend is reassuring, not proof. If product quality drifts, review pretreatment and operating data before changing settings; the root cause may sit upstream of the EDI module.
How EDI Systems Are Maintained and Updated in 2026
In 2026, maintaining an electrodeionization (EDI) system starts with its feed water, not the module cabinet. Keep reverse-osmosis permeate within the EDI unit’s specified limits for conductivity, hardness, silica, and temperature. Small changes matter. A rise in product-water conductivity may point to upstream membrane performance, changing flow, or an EDI fault. Record product resistivity, feed and concentrate flows, pressure drop, voltage, current, and temperature at consistent intervals. Trends reveal more than isolated readings.
Routine checks should include inspecting sample lines for leaks, confirming flow-meter readings, and reviewing alarms before resetting them. Calibrate conductivity and resistivity instruments on their scheduled cycle, using suitable standards and documented procedures. If scaling or fouling is suspected, confirm the feed-water data and consult the module’s operating guidance before cleaning. Guesswork can make things worse. Keep maintenance records tied to dates, readings, and specific actions; a tidy spreadsheet is not proof that every sensor is accurate.
System updates in 2026 may include replacing aging sensors, improving alarm thresholds, or updating control software. Test changes against operating records and verify that shutdowns, alerts, and data logging still work. Back up settings before changes. After an update, compare readings with an independent check where practical, then watch the system closely through its next operating cycle. Not every fluctuation needs intervention, and that judgment deserves review too.
How Does an EDI Water System Work in 2026? - How EDI Systems Are Maintained and Updated in 2026
| System stage | How it works | What operators monitor | Maintenance and updates in 2026 |
|---|---|---|---|
| Pretreatment and reverse osmosis (RO) | Pretreatment reduces suspended solids, oxidants, hardness, and other contaminants. RO then removes most dissolved salts and prepares low-conductivity feed for the EDI stage. | RO permeate conductivity, pressure, flow, recovery, and feed-water quality. EDI feed limits are system-specific; common design checks include low hardness, low silica, and no harmful residual oxidant. | Trend RO performance and differential pressure; inspect pretreatment equipment and replace consumables based on condition and validated service intervals. Confirm feed-water specifications against the EDI module documentation. |
| EDI feed conditioning | RO permeate enters the EDI module. Flow distribution and, where installed, carbon dioxide management help keep the feed within the module's operating envelope. | Feed conductivity, temperature, flow, pressure, hardness, silica, and carbon dioxide or alkalinity where relevant. | Investigate changes in feed quality before adjusting the EDI module. Check instruments against calibration schedules and review alarms for recurring deviations. |
| Ion removal inside the EDI module | An applied direct-current field moves cations and anions through selective ion-exchange membranes into concentrate channels. Ion-exchange resin in the dilute compartments supports ion transport and removal. | Product-water resistivity or conductivity, voltage, current, dilute and concentrate flow, pressure drop, and module temperature. | Compare trends with the module's approved operating limits. A rising product conductivity or unusual electrical reading can indicate feed-quality, hydraulic, instrumentation, or module issues; diagnose before changing settings. |
| Continuous electrical regeneration | The electric field helps split water into hydrogen and hydroxide ions. These ions continually regenerate the resin, so routine acid-and-caustic regeneration is generally not part of normal EDI operation. | Stable current and voltage, correct flow, product quality, and safe handling or venting of gases as specified by the system design. | Do not apply chemical cleaning or regeneration unless the module supplier's approved procedure requires it. Follow electrical isolation and safety procedures for inspection or service. |
| Product-water monitoring and storage | EDI product water is monitored and routed to the point of use or a suitable storage and distribution loop. Downstream treatment may be needed for particular applications. | Conductivity or resistivity, temperature-compensated readings where appropriate, flow, and application-specific quality tests. | Verify sensor calibration and sample-point suitability. Assess storage and distribution hygiene separately; EDI alone does not guarantee microbial control throughout a water system. |
| Routine maintenance planning | Preventive maintenance protects feed quality, stable hydraulics, accurate monitoring, and reliable electrical operation. | Operating logs, alarms, calibration records, leaks, abnormal noise, flow balance, and changes in product quality or pressure drop. | Use a site risk-based schedule: review operating trends routinely, inspect equipment at planned intervals, and service filters, instruments, pumps, and valves according to measured condition and documented requirements. Intervals depend on water quality and system design. |
| Controls and software updates | The control system monitors process values, runs alarms and interlocks, and may record operating data for troubleshooting and quality review. | Alarm history, data gaps, sensor status, control logic, access permissions, and communication faults. | Treat firmware, software, and cybersecurity changes as controlled changes: back up configurations, assess impact, test where practical, document approval, and verify alarms and interlocks after implementation. Install only compatible, validated updates. |
| Performance troubleshooting | EDI performance depends on suitable feed quality, correct flow and pressure, stable electrical operation, and reliable measurement. | Compare current readings with the site's baseline and the module's specified limits; check whether the change is gradual, sudden, or linked to an upstream event. | Check instruments and feed-water conditions first, then hydraulic and electrical factors. Record findings and involve qualified service personnel if performance remains outside approved limits; avoid unsupported set-point changes. |
Operating limits and service intervals vary by module, system design, feed-water composition, and application. Use the applicable technical documentation and site procedures for final operating and maintenance decisions.